What the station does
The ingot drops out of the mould, is weighed and gets its heat mark, shown at millimetre scale.
A buyer checks two things first: a sound ingot of the right mass and a readable heat mark. Both depend on millimetres: where the knocker strikes, how the scale lifts the ingot, how close the marking pin is. The station is specified with every device at its true datasheet size.
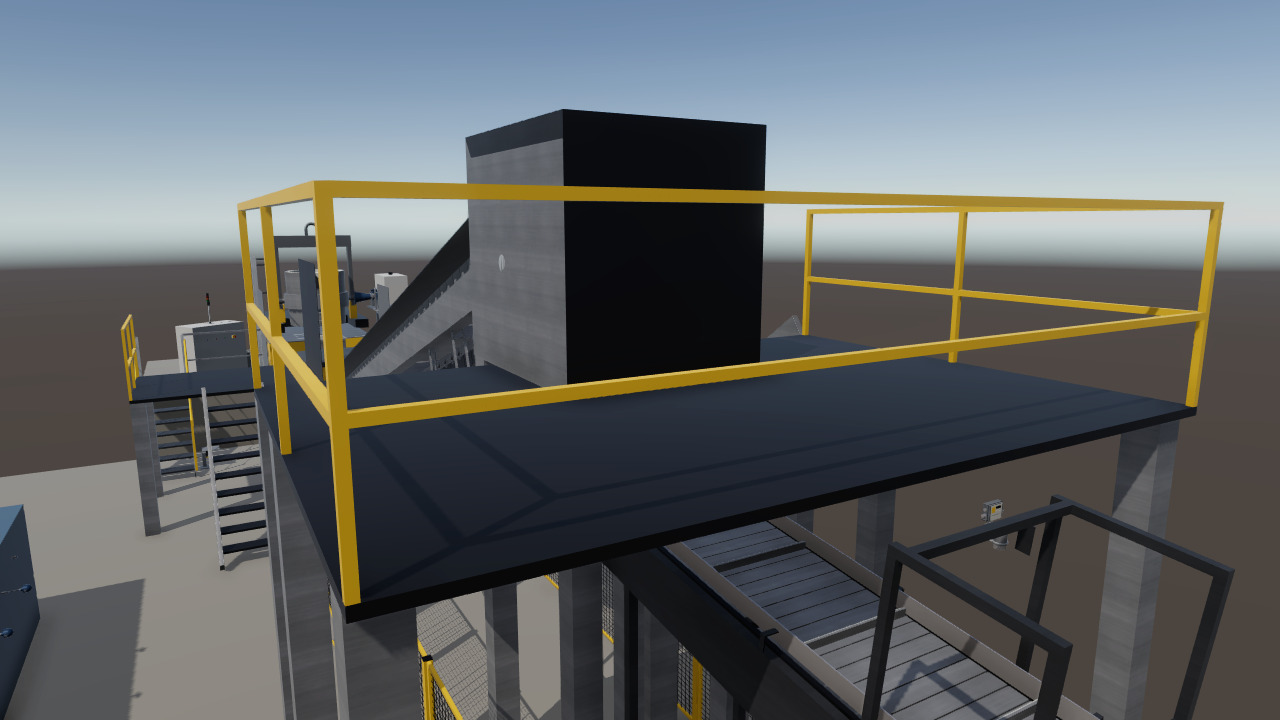
Step by step
- A pulse per mould tells the tracking the heat and number of each ingot.
- At the head, the mould turns over, and a knocker strikes it once.
- A light beam sees the drop, and a sensor checks the empty mould.
- After cooling, a plate lifts the ingot onto four weight sensors.
- Good ingots weigh 19.5 to 22.0 kg and are at 150 °C or below.
- Each good ingot is clamped and marked in about 3 s.
Specifications
The devices
Each device is a real catalogue product. Its own product page will follow on the products level.
| Device | Role |
|---|---|
| Inductive proximity sensor | Gives one pulse per mould on the chain. |
| Through-beam light sensors | Light beams for the drop and short ingots. |
| Pyrometer, 385 to 1,600 °C | Reject flag above 700 °C after the drop. |
| Load cells (4 x 50 kg) | Weigh each ingot to about 67 g. |
| Pneumatic cylinders with valves | Weigh lift, reject pusher, marker stop and clamp. |
| Dot-peen marking unit | Stamps the heat and sequence number. |
Links lead to the makers' public product pages and are given for reference only. This site is independent work, not affiliated with, sponsored or endorsed by any manufacturer. The makers are responsible for the content of their pages. Trademarks belong to their owners.
The signals
| Signal | Direction | Meaning |
|---|---|---|
| Mould index | to PLC | One pulse per mould. |
| Ingot on chute | to PLC | Ingot must cross the beam within 3 s. |
| Ingot still in mould | to PLC | An ingot here means a jam. |
| Ingot mass | to PLC | Net mass, accepted at 19.5 to 22.0 kg. |
| Clamp closed | to PLC | The marker starts only with this signal. |
| End of marking | to PLC | No pulse within 6 s raises an alarm. |
About this page
In the scenario, this station gives every 16 Psyche ingot its weight and its heat mark before it leaves for bundling.
Real devices, built from real data
Every machine and device in this twin is a real industrial product from the makers' catalogues. They range from sensors, valves and drives to safety scanners, load cells and RFID readers. Each model is built from the product's published data: dimensions, sensing ranges, signals, rated values, parameters and timing.
The PLC programs use the devices' real interfaces and parameters. Before any hardware existed, the twin found hundreds of faults in the plant design and the programs. So a real commissioning would need fine tuning, not a redesign.